Royal Apollo Group: The role of spiral conveyors in warehousing and logistics
Supplier News
In the dynamic world of warehousing and logistics, efficiency, space utilization and speed are paramount. Businesses are constantly seeking innovative solutions to streamline their operations and meet the ever-growing demands of the supply chain. Spiral conveyors have emerged as a pivotal technology, offering numerous benefits that transform warehousing and logistics processes. This blog explores the critical role that spiral conveyors play in enhancing operational efficiency and optimizing space in modern warehouses and logistics centers.
Optimizing space utilization
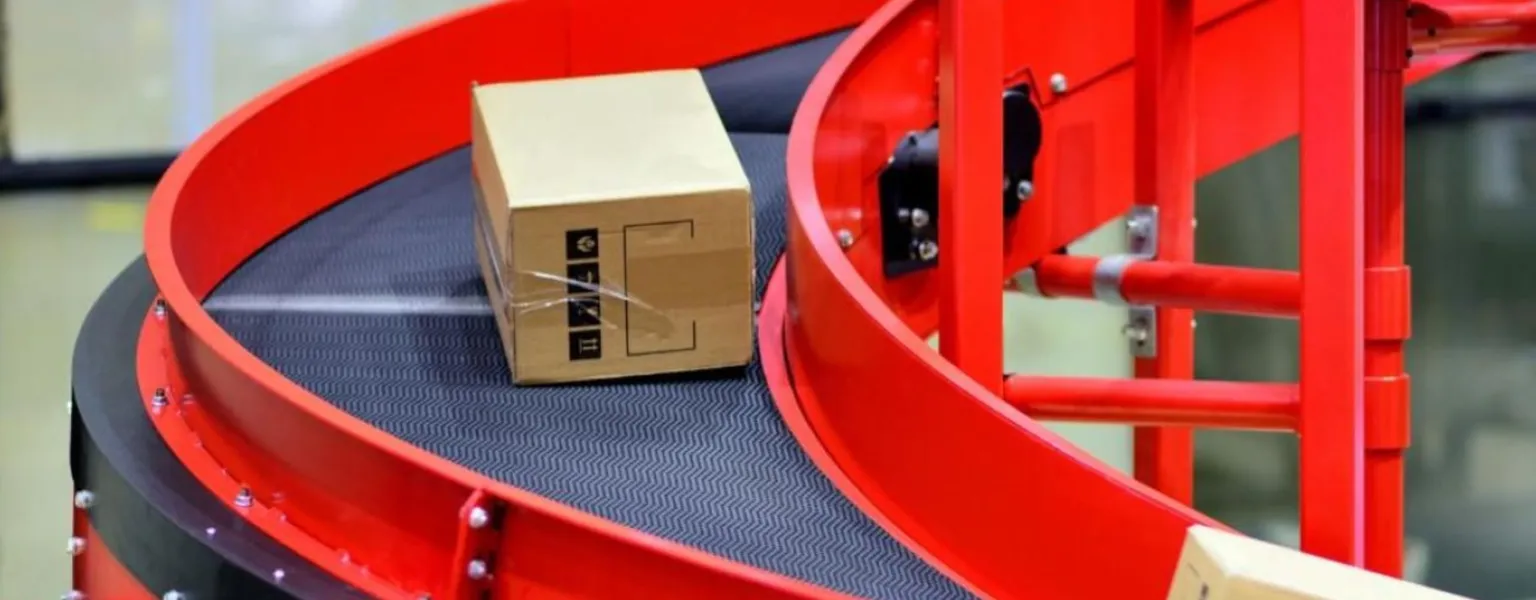
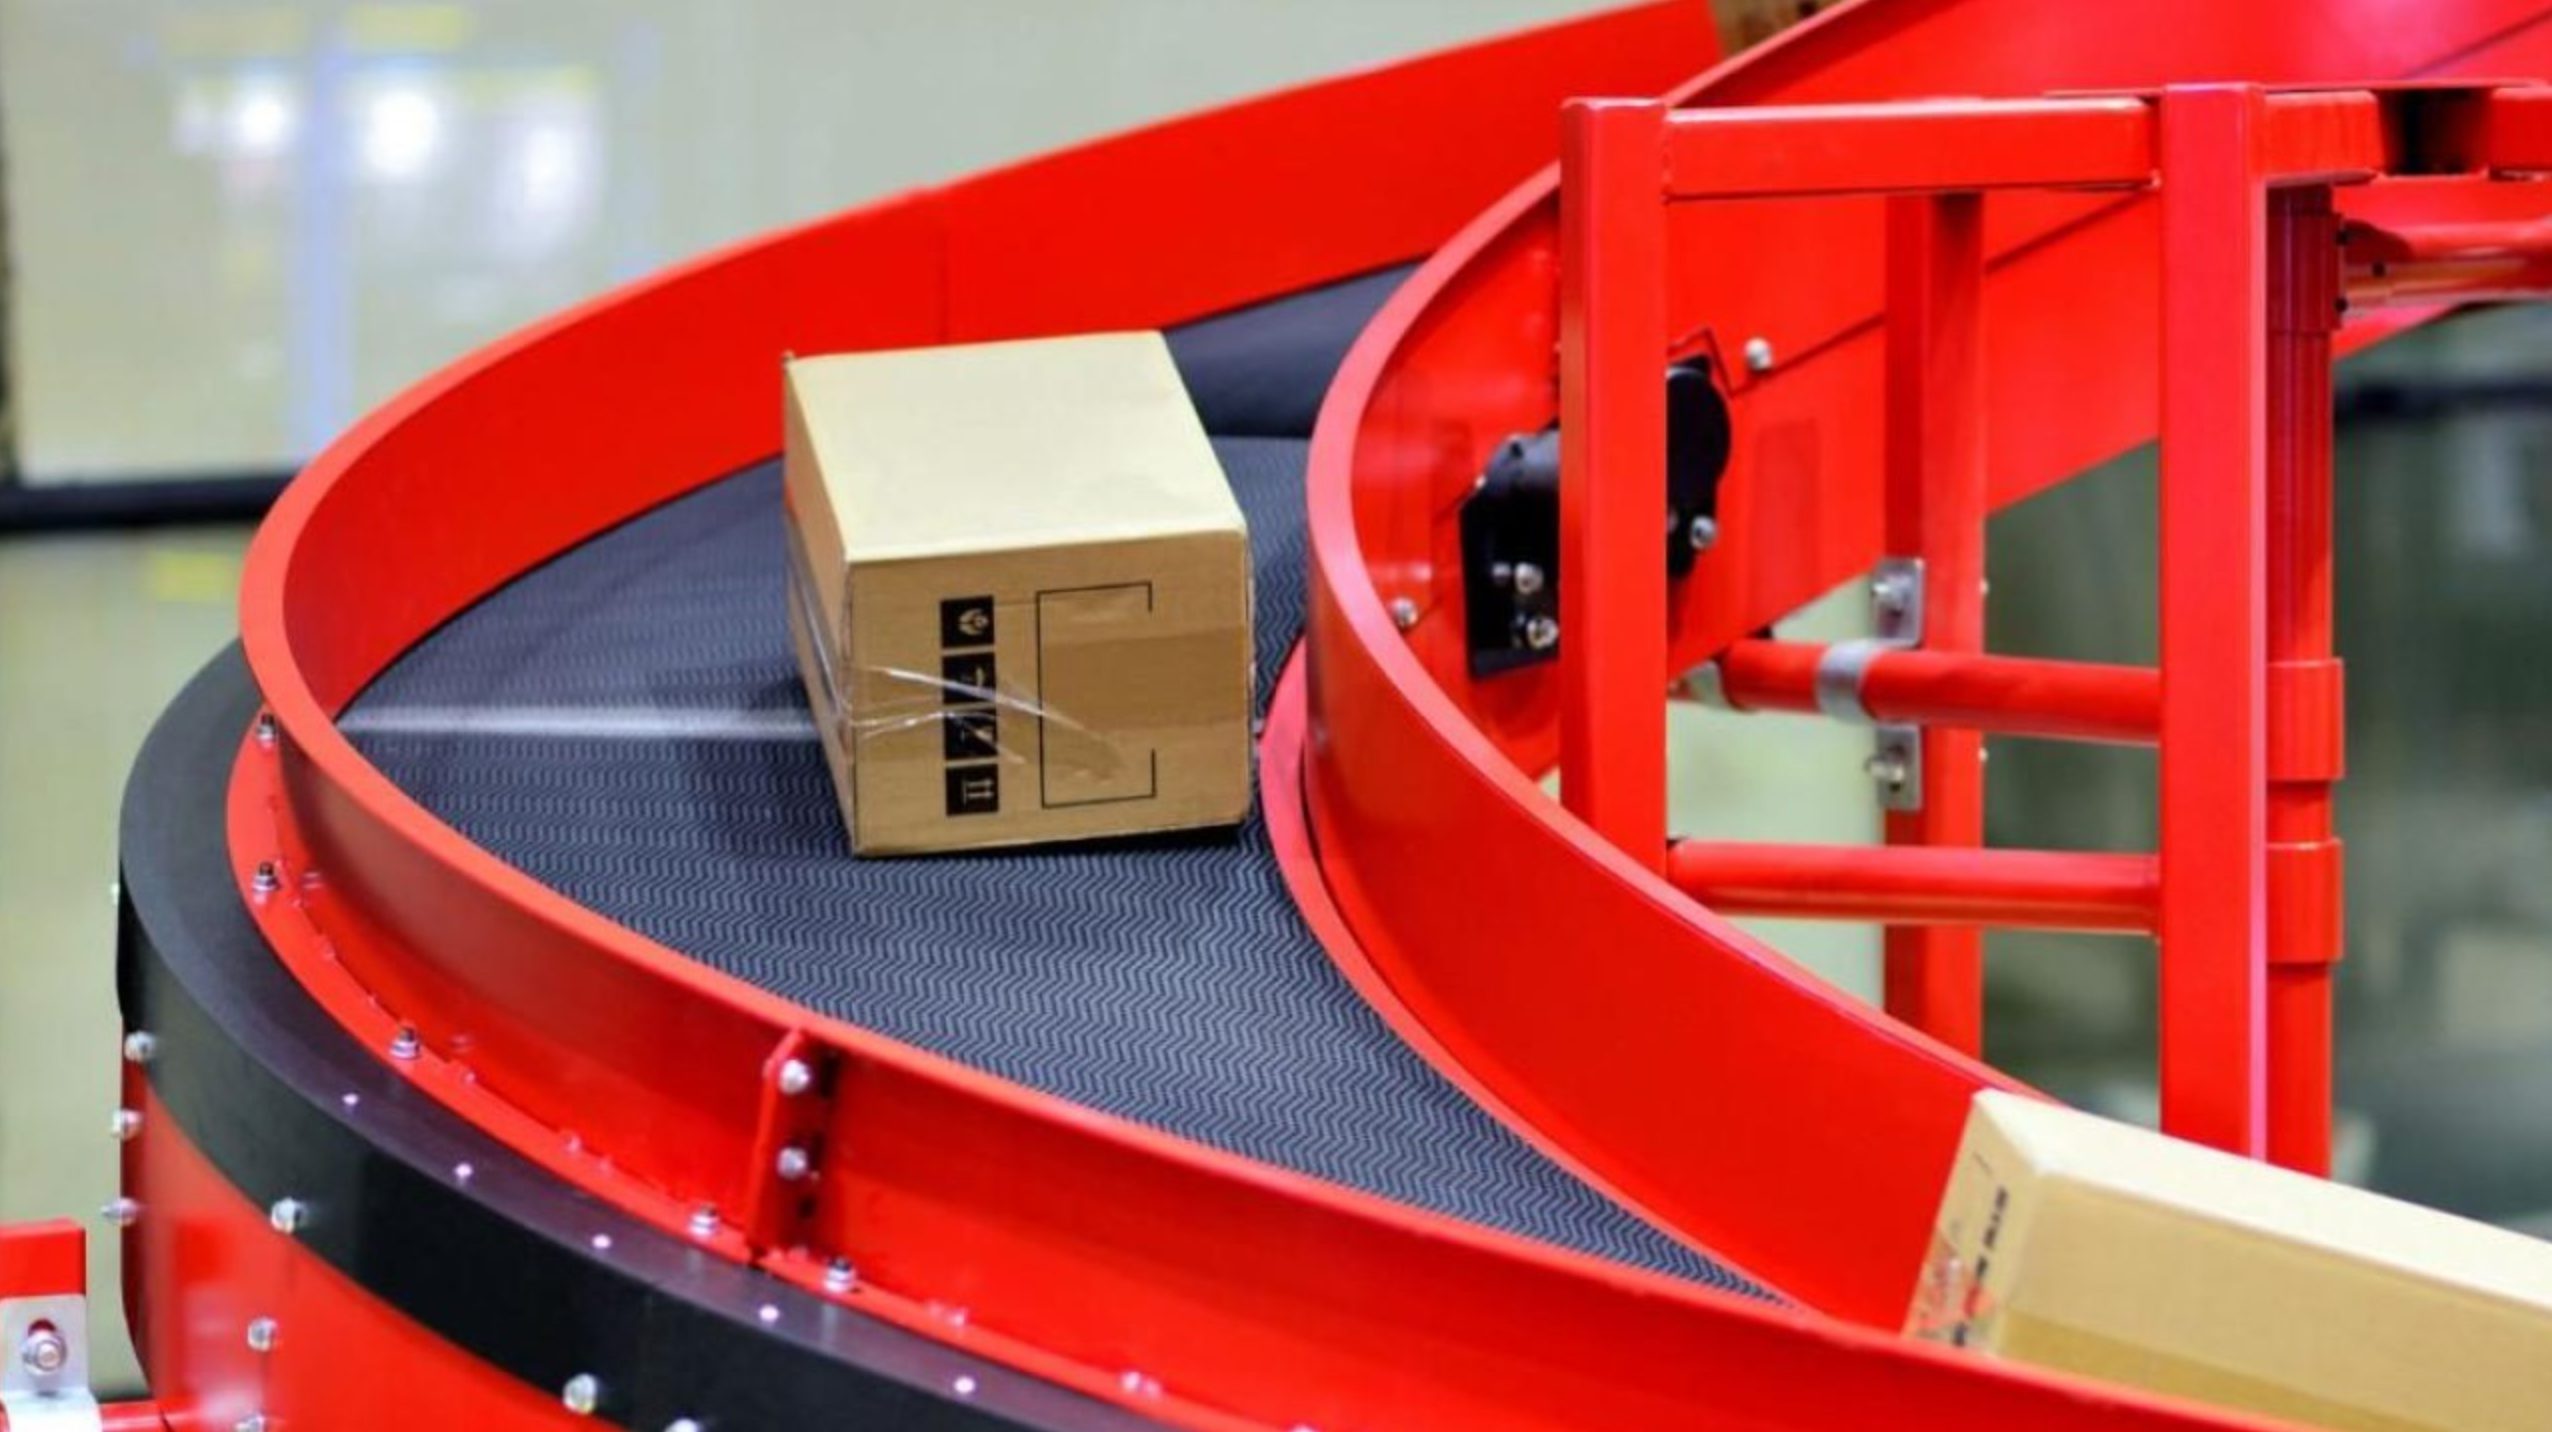
One of the primary advantages of spiral conveyors is their ability to maximize space utilization. Traditional conveyor systems require extensive horizontal space, which can limit the capacity and efficiency of a warehouse. Spiral conveyors, on the other hand, use vertical space effectively. By moving products upwards or downwards in a compact spiral configuration, these conveyors free up valuable floor space for storage, picking, packing and other operational activities. This is particularly beneficial in urban warehouses where space is often limited and expensive.
Enhancing operational efficiency
Efficiency is crucial in warehousing and logistics, where the speed of processing and moving goods directly impacts the bottom line. Spiral conveyors facilitate the smooth and continuous flow of products between different levels of a facility, reducing bottlenecks and improving overall throughput. Their seamless integration with existing conveyor systems ensures that goods move swiftly and efficiently from one point to another. This enhanced efficiency leads to faster order fulfillment, reduced lead times and increased customer satisfaction.
Flexibility and versatility
Spiral conveyors are known for their versatility. They can handle a wide range of products, from small parcels to large packages, making them suitable for various industries, including e-commerce, manufacturing, food and beverage, and pharmaceuticals. Their adaptability allows businesses to customize the conveyor system to meet their specific needs. Whether it's transporting goods between floors, connecting different sections of a warehouse, or integrating with automated systems, spiral conveyors offer the flexibility required to optimize logistics operations.
Improving safety and reducing labor costs
Automation is a key driver in enhancing safety and reducing labor costs in warehousing and logistics. Spiral conveyors automate the vertical transportation of goods, eliminating the need for manual lifting and carrying, which can be hazardous and labor-intensive. By reducing manual handling, spiral conveyors minimize the risk of workplace injuries and improve overall safety. Additionally, automation reduces reliance on manual labor, leading to lower operational costs and allowing staff to focus on more value-added tasks.
Three types of spiral conveyors typically designed for warehousing & logistics
1. Wide trak
The ROYAL Apollo largest Spiral features the widest conveying surface and has gained rapid adoption in venues like home improvement stores, accommodating diverse product sizes and heavy SKUs. With an industry-leading conveying surface width up to 900 mm., our Wide Trak models offer exceptional performance for large products.
2. Heavy duty
The Heavy Duty models are tailored for heavier loads and offer customizable conveying with a load capacity of 100 kg per meter and speeds up to 60 meter per minute. The innovative chain-slat arrangement allows seamless transport of various unit sizes without the hassle of adjustments, making it ideal for dynamic operations like pick modules where package sizes vary widely.
3. Multiple entry & exit
Our Heavy Duty models offer optional shoot-in or shoot-out capabilities at intermediate levels. The unique shoot-in/out conveyors feature individually adjustable surfaces to seamlessly match the Spiral's pitch, ensuring safe and reliable product transfers.
Conclusion
Royal APOLLO Spiral conveyors are revolutionizing the warehousing and logistics industry by offering solutions to some of its most pressing challenges. Their ability to optimize space, enhance operational efficiency, improve safety and reduce labor costs makes them an invaluable asset for any modern warehouse or logistics center. As the industry continues to evolve, spiral conveyors will undoubtedly remain at the forefront of material handling innovation, driving businesses towards greater productivity and success. By incorporating spiral conveyors into their operations, warehousing and logistics companies can achieve significant improvements in efficiency, space utilization and overall performance, positioning themselves for success in an increasingly competitive market.
This article was originally published by Royal Apollo Group.

Related News
-
Supplier News
Royal Apollo Group joins Interroll Holding AG
-
Supplier News
Apollo VTS Asia showcases at ProPak Asia 2025
-
Supplier News
Discover the power of Apollo’s multiple infeed & outfeed spiral conveyor
-
Supplier News
Royal Apollo Group: 5 signs you need a conveyor upgrade
-
Supplier News
Royal Apollo Group: Logistics systems to optimise material flow and operations
Latest Packaging News

Exchange for Change’s Julian Hunt discusses preparations for UK DRS
The UK's Deposit Return Scheme is moving rapidly from policy debate to operational reality. With...
Spanish sauce brand adopts bespoke flip top closure
Amcor has developed a new customized flip top closure for Spanish sauce brand Choví. The...
From regulation to solution: adapting to PPWR legislation with Boix
The Packaging and Packaging Waste Regulation (PPWR) is changing the packaging landscape across the...
OMAG: Liquid collagen packaging – precision and flexibility for every production need
Liquid collagen is increasingly used in the nutraceutical, cosmetic and food industries thanks to...